Application
HOME>Application
New Energy Sector

New Energy Sector

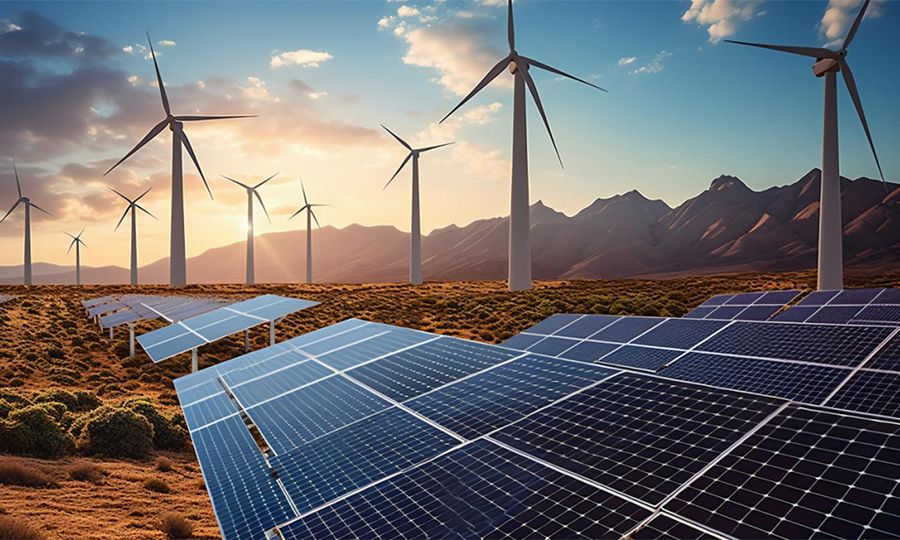
Chemical products in the new energy field are the core support of the industrial chain, mainly applied in three links: energy storage, power generation and energy conversion, which determine the performance, cost and safety of new energy products. 1. Energy storage field: The core lies in battery materials Energy storage is the key to the consumption of new energy. The performance of its core carriers, power batteries and energy storage batteries, is completely dependent on chemical materials. Cathode material: It determines the energy density of the battery. The mainstream ones are ternary materials (lithium nickel cobalt manganese oxide) and lithium iron phosphate, both of which are fine chemical synthesis products. Negative electrode materials: They affect the battery's cycle life, mainly artificial graphite and natural graphite, and need to undergo chemical processes such as purification and coating. Electrolyte: The "blood" of a battery, composed of lithium salts (such as lithium hexafluorophosphate), organic solvents (such as carbonates), and additives, is responsible for ion transport. Diaphragm: The key to preventing short circuits between the positive and negative electrodes. The mainstream is polyethylene and polypropylene microporous membranes, which need to be prepared through chemical techniques such as stretching and pore-forming. 2. Power generation field: Covering photovoltaic and wind power The efficiency improvement and equipment durability in the power generation process rely on chemical products with specific functions. In the photovoltaic field, the main applications are reflected in two aspects: photovoltaic glass encapsulation films. In the field of wind power, it is mainly reflected in two aspects: wind turbine blades and gear oil and grease.

View more

Plastics Industry

Plastics Industry

As an important pillar of modern materials industry, the development of the plastic industry cannot be separated from the support of various chemical products. From basic resin raw materials to functional additives, chemicals run through the entire process of plastic production and processing, determining the final performance and application areas of plastic products. The application of chemicals in the processing of different types of plastics The performance of plastic products depends not only on the type of base resin, but also closely related to the added chemicals and their processing technology. Due to the differences in molecular structure and performance characteristics of different types of plastics, specific chemical combinations need to be added in a targeted manner to meet the needs of various application scenarios. From general plastics to engineering plastics, from hard products to soft films, the precise application of chemicals has shaped the diversified product system of modern plastic industry. The application of chemicals in polyvinyl chloride (PVC) products. As a multifunctional plastic, PVCs processing and application rely heavily on various specialized chemicals. Pure PVC resin is prone to thermal degradation at high temperatures, releasing hydrogen chloride gas, leading to material discoloration and performance degradation. Therefore, heat stabilizers are essential in PVC processing. Traditionally, lead salt stabilizers have been used, but due to environmental and health considerations, lead-free stabilizers such as calcium zinc (Ca/Zn) composite stabilizers have gradually become mainstream choices, especially in the field of building materials such as PVC pipes. Plasticizers are a key component of soft PVC products, with an addition amount of up to 30% -50% of the resin weight. Phthalate plasticizers such as di (2-ethylhexyl) phthalate (DEHP) have long dominated the PVC plasticizer market due to their excellent performance and cost-effectiveness, and are widely used in medical catheters, wires and cables, and other fields. However, due to health hazards, regions such as Europe and America have gradually restricted the application of certain phthalates in sensitive fields, promoting the development of new plasticizers such as citrate esters and polyesters.     PVC processing also requires the assistance of lubricants, as PVC melt has high viscosity and poor fluidity, which can easily lead to processing difficulties. Proper addition of lubricants can improve melt flowability, reduce processing temperature, and increase production efficiency. According to different mechanisms of action, PVC lubricants are divided into internal lubricants (such as stearic acid) and external lubricants (such as PE wax), which together ensure the smooth flow of PVC melt during extrusion or injection molding without adhering to equipment. In the formulation design of PVC pipes, the use of fillers (such as calcium carbonate) should also be considered to reduce costs, while adding appropriate amounts of impact modifiers (such as CPE, MBS) to improve the low-temperature toughness of the pipes and meet the requirements of building materials standards. Optimization of Chemicals in Polyolefin (PE/PP) Products: Polyethylene (PE) and polypropylene (PP), as the most abundant polyolefin plastics, cannot be processed and applied without the combination of various functional chemicals. Polyolefins are prone to oxidative degradation during processing and use, therefore antioxidant systems are crucial. A typical formula includes a synergistic combination of primary antioxidants (such as hindered phenolic compound β - (3,5-di-tert-butyl-4-hydroxyphenyl) propionic acid octadecanol ester) and auxiliary antioxidants (such as triphosphate (2,4-di-tert-butylphenyl) ester), effectively capturing free radicals and decomposing peroxides, extending the service life of the product. For PE products that require outdoor use such as agricultural film, light stabilizers such as hindered amines (HALS) need to be added to resist the destructive effects of ultraviolet rays in sunlight, significantly extending the service life of the film.     The transparency of PP plastic is usually poor, and adding nucleating agents can promote PP crystallization refinement, improve its transparency and surface gloss. Sorbitol derivatives are highly efficient PP nucleating agents that can achieve a transparent effect similar to polystyrene in PP products, and are widely used in food packaging and medical devices. PP is also prone to static electricity accumulation. Adding anti-static agents such as glycerol monostearate can reduce surface resistance and prevent dust adsorption, which is particularly important in electronic product packaging. For PP parts used in automobiles, it is usually necessary to add fillers such as talcum powder to improve rigidity and heat resistance, while also using elastic toughening agents to improve low-temperature impact resistance and meet the stringent requirements of automotive environments. Engineering plastics and high-performance additives. Engineering plastics such as ABS, PC, PET, etc. have stricter requirements for additives and need to maintain stable performance under harsh conditions such as high temperature and high stress. Due to the presence of butadiene components, ABS plastic has relatively poor weather resistance and is prone to yellowing and brittleness during outdoor use. Therefore, efficient UV absorbers such as benzotriazole compounds need to be added in combination with antioxidants to significantly improve the durability of ABS in applications such as automotive and electronic casings. Although PC plastic has excellent impact resistance, it is prone to hydrolysis during processing and must undergo strict drying, sometimes requiring the addition of hydrolysis stabilizers; Meanwhile, the scratch resistance of PC is limited, and adding appropriate scratch resistant agents such as silicone compounds can improve its surface properties, making it suitable for high-end applications such as eyeglass lenses and electronic displays.     PET plastic dominates in the fields of beverage bottles and fibers, and its processing requires controlling the crystallization rate. Adding appropriate nucleating agents can regulate the crystallization behavior of PET, improve the formability of bottle preforms, and ultimately enhance the transparency of the bottle. For flame-retardant engineering plastics such as flame-retardant ABS, flame-retardant PC, etc., efficient flame retardant systems such as bromine antimony synergistic systems or phosphorus based flame retardants need to be added to meet the strict fire protection requirements of electronic and electrical products. The application of coupling agents (such as silane coupling agents) is crucial in fiberglass reinforced engineering plastics, as it can improve the interfacial bonding between fiberglass and resin matrix, significantly enhancing the mechanical strength of composite materials.   Table: Key Additives and Their Functions for Major Plastic Types; Plastic typeKey additives Main functions Typical applications PVC Heat stabilizers, plasticizers Prevent thermal degradation and increase flexibility Pipes, cables, medical products PE Antioxidants, light stabilizers Prevent oxidation and ultraviolet degradation Plastic film, packaging, pipes PP Nucleating agent, antistatic agent Enhance transparency and prevent static electricity Food packaging, electronic components Engineering plastics Coupling agent, flame retardant Enhance mechanical performance and improve fire resistance Automobile parts, electronic appliances

View more

Agriculture and Special Applications

Agriculture and Special Applications

As an important foundation of modern industry, chemical products have deeply penetrated into the two key fields of energy and medicine, not only promoting technological progress, but also reshaping the industrial landscape.   1、 Energy sector: From traditional fuels to green materials   Refining and upgrading traditional energy sources   Petrochemical production of traditional fuels such as gasoline and diesel through refining technology remains the core of energy supply. But in recent years, chemical technology has focused more on the efficient utilization of energy and low-carbon transformation. For example, coal chemical industry converts coal into clean fuels such as methanol and olefins through gasification and liquefaction technologies, reducing pollution from direct combustion  。 Yulin, Shaanxi Province converts coal into biodegradable materials such as polyglycolic acid (PGA) through the coal to olefin industry chain, which are used for medical sutures and photovoltaic panel components   2、 Chemical support for new energy materials   Lithium batteries and photovoltaic materials: Ethylene and propylene derived from petrochemicals are key raw materials for lithium battery electrolytes and separators; Coal based PGA can be further processed into photovoltaic grade EVA resin for packaging solar panels.   Hydrogen energy and carbon cycle: Chemical technology supports the development of the hydrogen energy industry chain, such as Yulins promotion of the hydrogen fuel cell heavy-duty truck project; Carbon dioxide capture technology converts industrial waste gas into new energy materials, forming a negative carbon industry chain.   3、 Energy saving and environmental protection technologies   Modern coal chemical industry reduces energy consumption and promotes low-carbon industries through water recycling (such as concentrated salt water reuse devices) and waste gas recovery Backup application scenario:   Agriculture and Special Uses   fine chemicals   Medical and daily necessities   High tech field:

View more
Energy and Pharmaceuticals

Energy and Pharmaceuticals

As an important foundation of modern industry, chemical products have deeply penetrated into the two key fields of energy and medicine, not only promoting technological progress, but also reshaping the industrial landscape.   1、 Energy sector: From traditional fuels to green materials   Refining and upgrading traditional energy sources   Petrochemical production of traditional fuels such as gasoline and diesel through refining technology remains the core of energy supply. But in recent years, chemical technology has focused more on the efficient utilization of energy and low-carbon transformation. For example, coal chemical industry converts coal into clean fuels such as methanol and olefins through gasification and liquefaction technologies, reducing pollution from direct combustion  。 Yulin, Shaanxi Province converts coal into biodegradable materials such as polyglycolic acid (PGA) through the coal to olefin industry chain, which are used for medical sutures and photovoltaic panel components   2、 Chemical support for new energy materials   Lithium batteries and photovoltaic materials: Ethylene and propylene derived from petrochemicals are key raw materials for lithium battery electrolytes and separators; Coal based PGA can be further processed into photovoltaic grade EVA resin for packaging solar panels.   Hydrogen energy and carbon cycle: Chemical technology supports the development of the hydrogen energy industry chain, such as Yulins promotion of the hydrogen fuel cell heavy-duty truck project; Carbon dioxide capture technology converts industrial waste gas into new energy materials, forming a negative carbon industry chain.   3、 Energy saving and environmental protection technologies   Modern coal chemical industry reduces energy consumption and promotes low-carbon industries through water recycling (such as concentrated salt water reuse devices) and waste gas recovery Backup application scenario:   Agriculture and Special Uses   fine chemicals   Medical and daily necessities   High tech field:

View more
Chemical Synthesis

Chemical Synthesis

From petrochemical raw materials to high value-added fine chemicals, from traditional synthesis methods to green and sustainable processes, the application of chemicals continues to drive innovation and progress in chemical synthesis technology. The core role of basic petrochemical raw materials in chemical synthesis The basic raw materials of petrochemicals constitute the backbone network of chemical synthesis, among which the olefin and aromatic hydrocarbon families are particularly important. Alkene compounds such as propylene, butene, and butadiene, as well as aromatic compounds such as benzene, toluene, and xylene, can be derived into thousands of chemical products through a series of chemical reactions, forming a vast system of modern chemical industry. These basic raw materials are like those in the chemical industry; Lego bricks; By using different combinations and conversion methods, specialized chemicals that meet the needs of various fields can be constructed.     Diversified applications of carbon three carbon four olefins: propylene, as the most important carbon three olefin, has applications far beyond the synthesis of polypropylene. Through ammonia oxidation reaction, propylene can be converted into acrylonitrile, which is a key monomer for the production of important materials such as acrylic fiber, nitrile rubber, ABS resin, etc.     The isopropylbenzene generated by the alkylation reaction of propylene and benzene can be used to produce phenol and acetone through the isopropylbenzene process, which are the basic raw materials for resins, adhesives, and solvents, respectively. The value of C4 olefins (butene, isobutene, butadiene) should not be underestimated. Butadiene can be converted into eight carbon straight chain olefins through linear polymerization reaction, which can then be aldehyded and hydrogenated to obtain nonanol. This substance has a wide range of applications in the synthesis of fragrances, surfactants, lubricant additives, and other fields. It is worth mentioning that when cobalt complexes are used as catalysts, the dimerization, trimerization, and tetramer of butadiene can all become high-quality raw materials for the synthesis of higher alcohols and macrocyclic musk, providing important support for the spice industry.     The key conversion pathway of the aromatic hydrocarbon family: Benzene, as the most basic member of the aromatic hydrocarbon family, is used globally for the production of styrene, which is a monomer used in the manufacture of polystyrene plastics and other styrene copolymers   Another 15-18% of benzene is used for the production of cyclohexane (nylon precursor) and phenol, while benzene is also the starting point for the synthesis of important derivatives such as aniline, alkylbenzene, and maleic anhydride. Although toluene is commonly used as a solvent in direct applications such as paints, inks, resins, etc., its value as a synthetic intermediate is more prominent. Through a series of reactions, toluene can be converted into products such as benzoic acid, benzyl chloride, meta cresol, and toluene diisocyanate (TDI), which further become key raw materials for pesticides, pharmaceuticals, and polyurethane materials. The three isomers of xylene (ortho, meta, and para) also have their own characteristics, especially the terephthalic acid produced by the oxidation of xylene, which is an irreplaceable raw material for the production of polyester fibers and plastics (such as PET).   Table: Main Petrochemical Basic Raw Materials and Their Derivative Products Basic raw materialsMain derivatives Application field Propylene Acrylonitrile, isopropylbenzene, propylene oxide Synthetic fibers, rubber, plastics, resins Butadiene Nonanol, higher alcohols, macrocyclic musk Spices, surfactants, lubricating oil additives benzene Styrene, cyclohexane, phenol Plastic, nylon, resin, adhesive Toluene Benzoic acid, TDI, m-cresol Pesticides, pharmaceuticals, polyurethane materials Reaction mechanism and process optimization: The conversion of these basic raw materials involves multiple catalytic mechanisms and reaction types. Taking the separation of isobutene as an example, due to its boiling point difference of only 0.6 ℃ with n-butene, chemical separation methods such as sulfuric acid extraction, adsorption separation, resin hydration dehydration are commonly used in industry, especially the methyl tert butyl ether (MTBE) cracking method, which is widely used. The purity requirements for isobutene also vary depending on the final product: producing MTBE, tert butanol, etc. requires a purity of over 50%; Preparation of methyl methacrylate (organic glass raw material) requires a purity of over 90%; The synthesis of butyl rubber requires over 99% high-purity isobutene. The precise control of these reaction conditions and process routes demonstrates the scientific and technological essence of chemical product synthesis.

View more